 PET-SHEET.COM


PET Sheet Thickness Varies Across the Roll Width: What Should Buyers Accept?
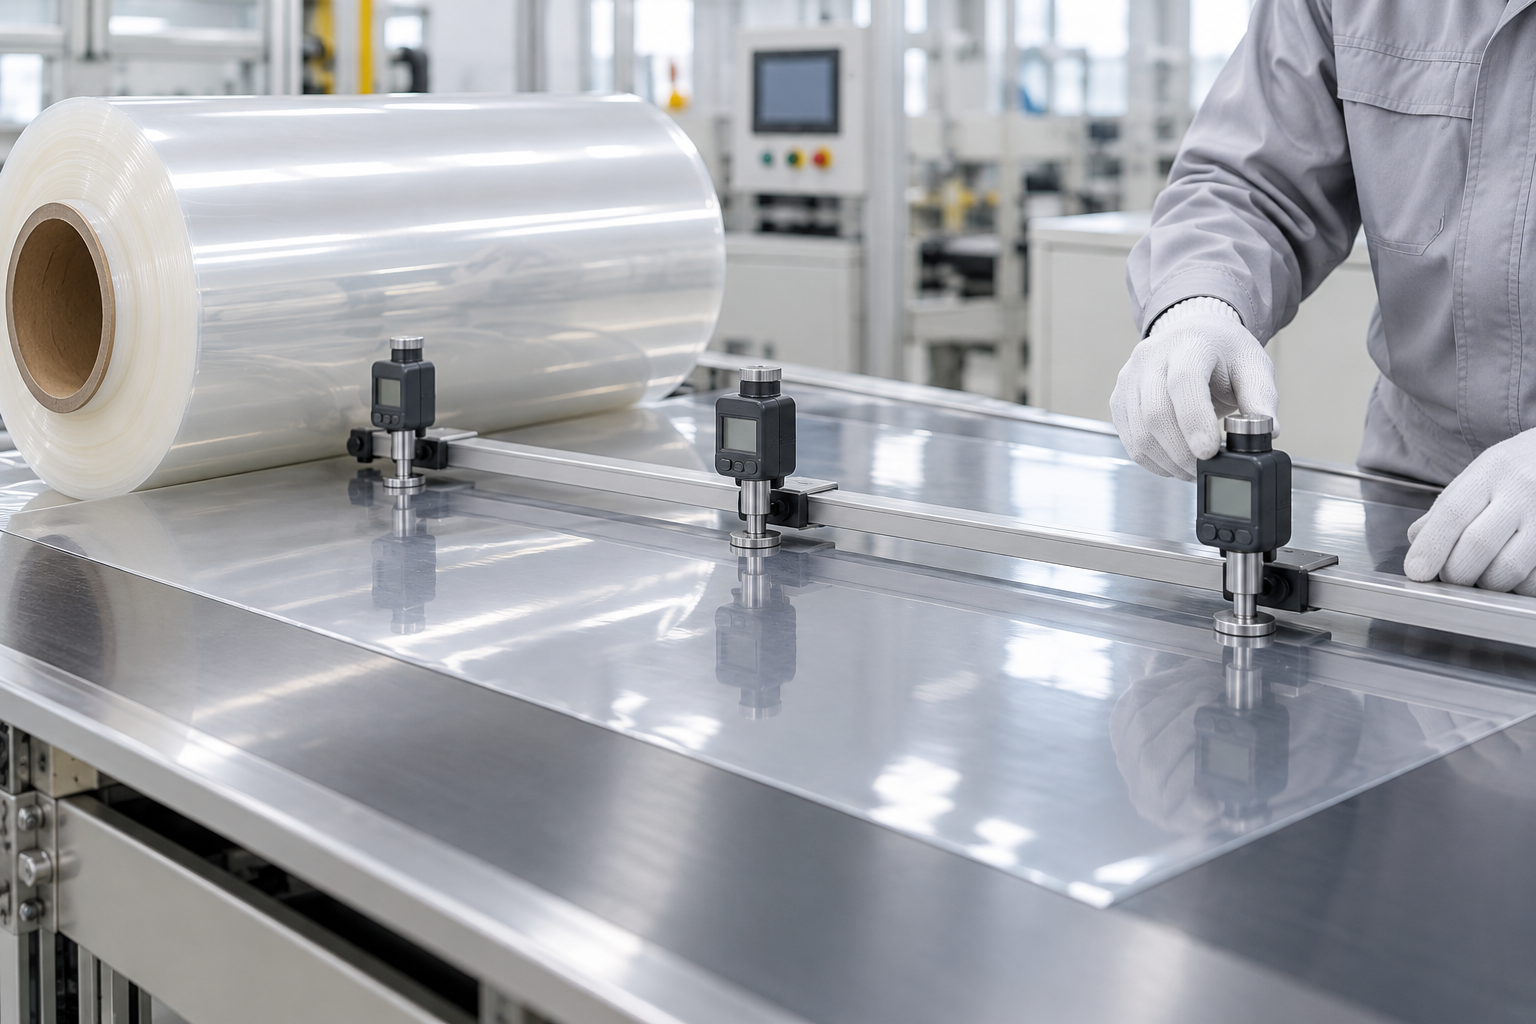
A PET roll arrives with the ordered gauge on its label. The centre reading looks acceptable, but measurements nearer one side are lower. The supplier points to the average thickness; your quality team is concerned about the packaging cavities that will run through that thinner area. Which result decides acceptance?
Neither the label nor one measurement settles the question. Acceptable variation needs to be defined across an agreed usable width, using an agreed measurement and sampling method, with limits connected to the packaging application.
We would start by asking where the variation sits relative to your packaging layout. That turns a disagreement about whether the sheet is “consistent” into a specification both parties can measure.
Distinguish nominal gauge, average thickness and the cross-width profile
These three descriptions answer different purchasing questions.
Nominal gauge is the thickness ordered. It identifies the target, but does not describe every location on the delivered sheet.
Average thickness summarises a defined set of readings. Its meaning depends on where and how those readings were taken. An average calculated from selected points is not automatically representative of the whole roll.
The cross-width profile shows thickness at identified positions across the sheet, perpendicular to the running direction. It preserves the location of higher and lower readings instead of combining them into one number.
A thicker area can offset a thinner area mathematically. The average may therefore sit close to nominal while a local band falls outside an agreed point limit. A centre reading misses that band entirely if it lies elsewhere across the width.
For purchasing acceptance, we recommend retaining the individual readings and their positions alongside any summary. Ask whether the reported result describes a single transverse sample, several samples along the roll, or a broader monitoring record. Those are different levels of evidence.
A profile at one location also cannot establish consistency throughout the roll length. Cross-width variation and changes along the running direction need separate coverage in the sampling agreement.
Connect local sheet variation to the packaging requirements
The practical concern is how much material is available locally before forming. A thinner band passing through a cavity footprint provides less starting material there than a thicker band elsewhere. Its significance depends on the package geometry, layout and subsequent material distribution.
Consider an illustrative layout with several cavities across the web. A low-thickness band might pass through an outer cavity, through the space between cavities, or through material reserved for gripping and trimming. The same profile can have different consequences in those positions.
That does not mean a thin sheet location will map directly to a particular finished-part wall thickness. Heating, geometry and forming conditions also affect distribution. Sheet measurements support material acceptance; they do not guarantee tray rigidity, seal integrity or other finished-package performance.
Mark the cavity footprints, gripping areas, trim boundaries and any critical package features on the width layout. Use that drawing to explain why a local minimum matters. For a demanding package, application checks may be needed to establish suitable sheet limits, but the resulting purchase specification should remain measurable on the delivered rollstock.
Our preference is to investigate the local profile before increasing nominal gauge. A heavier order may add material across the entire web without adequately addressing the variation that caused concern. Conversely, a tighter profile requirement deserves consideration when it protects usable output or reduces material-related production risk.
Agree usable width, measurement conditions and sampling positions
Before comparing results, establish that both parties measured the same thing.
Delivered roll width and usable width are not necessarily identical. Define the usable region by its boundaries and intended function. If edge exclusions are permitted, state their dimensions and locations explicitly. An edge area used for gripping still needs to meet the requirements of that function; it should not disappear from the specification simply because it does not become part of a tray.
For PET sheet roll width and thickness acceptance, the following agreement is more useful than a general request for “tight tolerance.”
| Item to agree | What the specification should define | Purchasing concern addressed |
|---|---|---|
| Width reference | Delivered width, usable boundaries, permitted exclusions and a fixed reference edge | Different interpretations of which material is covered |
| Cross-width positions | Distances from the reference edge, spacing and coverage of application-critical areas | A centre-only check or widely spaced readings missing a local band |
| Sampling along the roll | Which rolls and length positions are checked, including routine and investigation sampling | One accessible outer sample being treated as evidence for the full delivery |
| Measurement method | Instrument type, calibration status, resolution, contact geometry and measuring force | Readings differing because the methods differ |
| Sample condition | Conditioning, temperature, clean contact surfaces, flatness and treatment of coatings or protective layers | Comparing sheet measured under different conditions |
| Reporting | Individual readings, position identifiers, units, summaries and roll identification | An average concealing the location or extent of variation |
A fixed number of points is not automatically sufficient. Sampling spacing needs to reflect the width and the size of variation that matters to the application. If a narrow band is suspected, a closer investigation around that area may be appropriate in addition to the routine plan.
Do not pull a curled sample flat under uncontrolled tension or measure over a fold and assume the result represents normal sheet thickness. Agree how samples are prepared and supported. For surface-treated PET, also establish what the measured thickness includes so that incoming inspection and supplier inspection remain comparable.
We would resolve method differences before arguing over a borderline result. Instrument resolution, repeatability and rounding become particularly relevant when a reading is close to an acceptance boundary.
Discuss supplier profile monitoring, batch records and nonconforming rolls
Once the method is clear, ask what evidence will accompany repeat deliveries. “Thickness checked” provides little purchasing assurance unless the check can be connected to the supplied rolls.
Useful questions for a PET sheet supplier include how the profile is monitored, how often measurements are recorded, how results are linked to rolls, and what happens when a result moves outside the agreed limits. If continuous or scanning measurement is offered, clarify its coverage and how reported results relate to the delivered, trimmed or slit width. If control relies on periodic samples, clarify the gaps between those checks.
Neither approach should be accepted on its name alone. The relevant issue is whether its coverage and records support your purchase requirements.
Request identifiable profile records that retain the measurement positions, date or production reference, roll or lot identification, and disposition of any exception. Where parent rolls are slit, ask how the delivered roll is mapped to the parent profile. Otherwise, a record may show a width that does not correspond to the roll on your machine.
We recommend keeping the approved specification and representative qualification records as the baseline for repeat orders. A good sample establishes what was supplied for that sample; repeat records help assess consistency over time.
Agree the response to a nonconforming result before shipment. This can include holding the affected roll, confirming the measurement, checking the extent of the variation and deciding whether to replace, return or consider it for a specifically approved alternative use. Any concession should identify the affected material and its conditions of use. It should not silently become the standard for the next order.
Define mutually agreed acceptance limits
There is no useful universal tolerance to insert into every PET roll order. The agreed limits need to suit the gauge, usable width, sheet construction, packaging requirements and measurement method, while remaining achievable for the selected supply arrangement.
Separate the acceptance criteria rather than hiding everything behind one percentage:
- The nominal gauge and any permitted deviation of the defined average.
- Local minimum and maximum thickness within the specified region.
- Any limit on cross-width spread, with its calculation defined.
- Sampling coverage, retest rules and treatment of borderline results.
- Roll or lot disposition when a criterion is not met.
If percentage limits are used, identify the reference value. A percentage relative to nominal gauge is different from one calculated against the measured average. Likewise, maximum-minus-minimum spread does not by itself establish whether the whole profile is above or below the ordered target.
A passing average should not override a failed local limit when both are contractual requirements.
Tighter limits may narrow sourcing options or affect the quotation. Ask the selected manufacturer to confirm feasibility for the required width, gauge, structure and surface condition. Compare PET sheet roll price per kg against the material you can actually use, including any additional trim or rejected output associated with an unsuitable profile.
Our recommendation is to purchase a defined, application-relevant profile rather than an undefined promise of uniformity. The acceptance document should let two competent inspectors reach the same decision from the same sample.
FAQ About PET Roll Thickness Consistency
Can roll weight confirm that thickness is consistent across the width?
No. Roll weight alone cannot show where material is distributed across the width. Even a mass-based average requires reliable dimensions and material assumptions, and it can still conceal local thin or thick bands. Use position-specific thickness measurements to assess the cross-width profile.
What if incoming inspection disagrees with the supplier’s thickness report?
Identify the roll and sample location, then compare measurement methods, conditioning, instruments, surface preparation and width references. Remeasure a retained or jointly identified sample using the agreed method. If the difference remains, follow the documented retest or independent measurement procedure before deciding the material’s disposition.
Can a roll with an out-of-limit edge be accepted after additional trimming?
Possibly, if the remaining width meets the application and all relevant acceptance requirements. Additional trimming changes usable yield and may affect machine compatibility, so confirm those consequences and the commercial treatment before accepting the roll under a written concession. The concession should apply only to the identified material.
Does an acceptable thickness profile qualify a replacement PET sheet for production?
No. The profile establishes only the thickness criteria covered by the agreement. Formulation, surface condition and other sheet characteristics can still affect suitability. Keep those requirements in the material specification and assess a replacement under application-relevant conditions before approving regular supply.
Share your required gauge, delivered and usable widths, packaging layout, surface requirements and purchasing needs with DESU. We can discuss a suitable PET sheet specification, the profile evidence needed for acceptance, and samples or a quotation for your project.
Related Articles
CONTACT PET-SHEET.COM
Our professional sales staff and technicians will determine the final characteristics of the product and material solution for the customer specific application and will provide the customer with a quote and a detailed time schedule, Please fill the form to contact our professional sales team.- Main Category
- APET Sheet Roll
- ESD Antistatic PET Sheet Roll
- GAG Sheet Roll
- PETG Sheet Roll
- RPET Sheet Roll
- Thermoforming PET Sheet Roll
- Latest Products