 PET-SHEET.COM


What Incoming Checks Matter for an RPET Sheet Repeat Order?
The first RPET sheet order ran acceptably, so purchasing places a repeat order against the same description and nominal gauge. When the new rolls arrive, their labels look correct and the surface appears normal. Yet the thermoforming team wants to know whether the material can go straight to the line.
That decision should not be based on the words “same RPET sheet” alone. A repeat order is acceptable when its identity, dimensions, appearance, roll condition and production behavior remain within the baseline approved for the actual package and machine. The purpose of incoming inspection is to confirm that connection before a full production run puts output, labor and delivery schedules at risk.
For PET sheet for thermoforming, we usually start with traceability and the agreed specification, then move to physical inspection and a controlled line confirmation. This sequence catches obvious errors early without pretending that an incoming check can predict every forming result.
Start With Lot and Roll Identity
Before unwrapping every roll, establish exactly what arrived. A delivery can match the purchase order quantity while still containing a material, structure, color or roll format that does not match the approved order.
Check each roll label and the accompanying delivery information against the purchase order, approved specification and supplier documents. At minimum, connect the following details:
- supplier and material description;
- purchase order or contract reference;
- production lot or batch identity;
- individual roll number, where used;
- agreed RPET structure or recycled-content target;
- nominal thickness and width;
- color or appearance designation;
- roll weight or length basis used for the order;
- winding direction, core and roll-format requirements; and
- quantity received.
The key is traceability, not paperwork volume. If a defect appears during forming, the team must be able to identify which roll was running, whether adjacent rolls came from the same lot and what changed from the approved baseline. A generic pallet label that cannot be connected to individual rolls makes a later investigation much harder.
Do not combine unidentified material with accepted stock simply because the sheet looks similar. Hold any roll with a missing, damaged or conflicting label until its identity is resolved. This is especially important when several PET or RPET constructions are stored in the same area.
A repeat order also needs a defined lot. If several production lots arrive in one shipment, treat that as relevant information rather than averaging the shipment into one result. Sampling and production feedback should remain connected to each represented lot.
Perform Incoming Checks Against the Agreed Specification
Once identity is confirmed, ask a more practical question: which incoming characteristics could prevent the roll from fitting the machine, forming the approved part or meeting the package’s appearance standard?
The answer depends on the project. A clear retail pack may place tight emphasis on color, haze, gels and scratches. Another operation may be more sensitive to thickness behavior, edge condition, winding or roll diameter. The inspection plan should reflect the failure modes that matter to the approved product.
Check dimensions before appearance debates
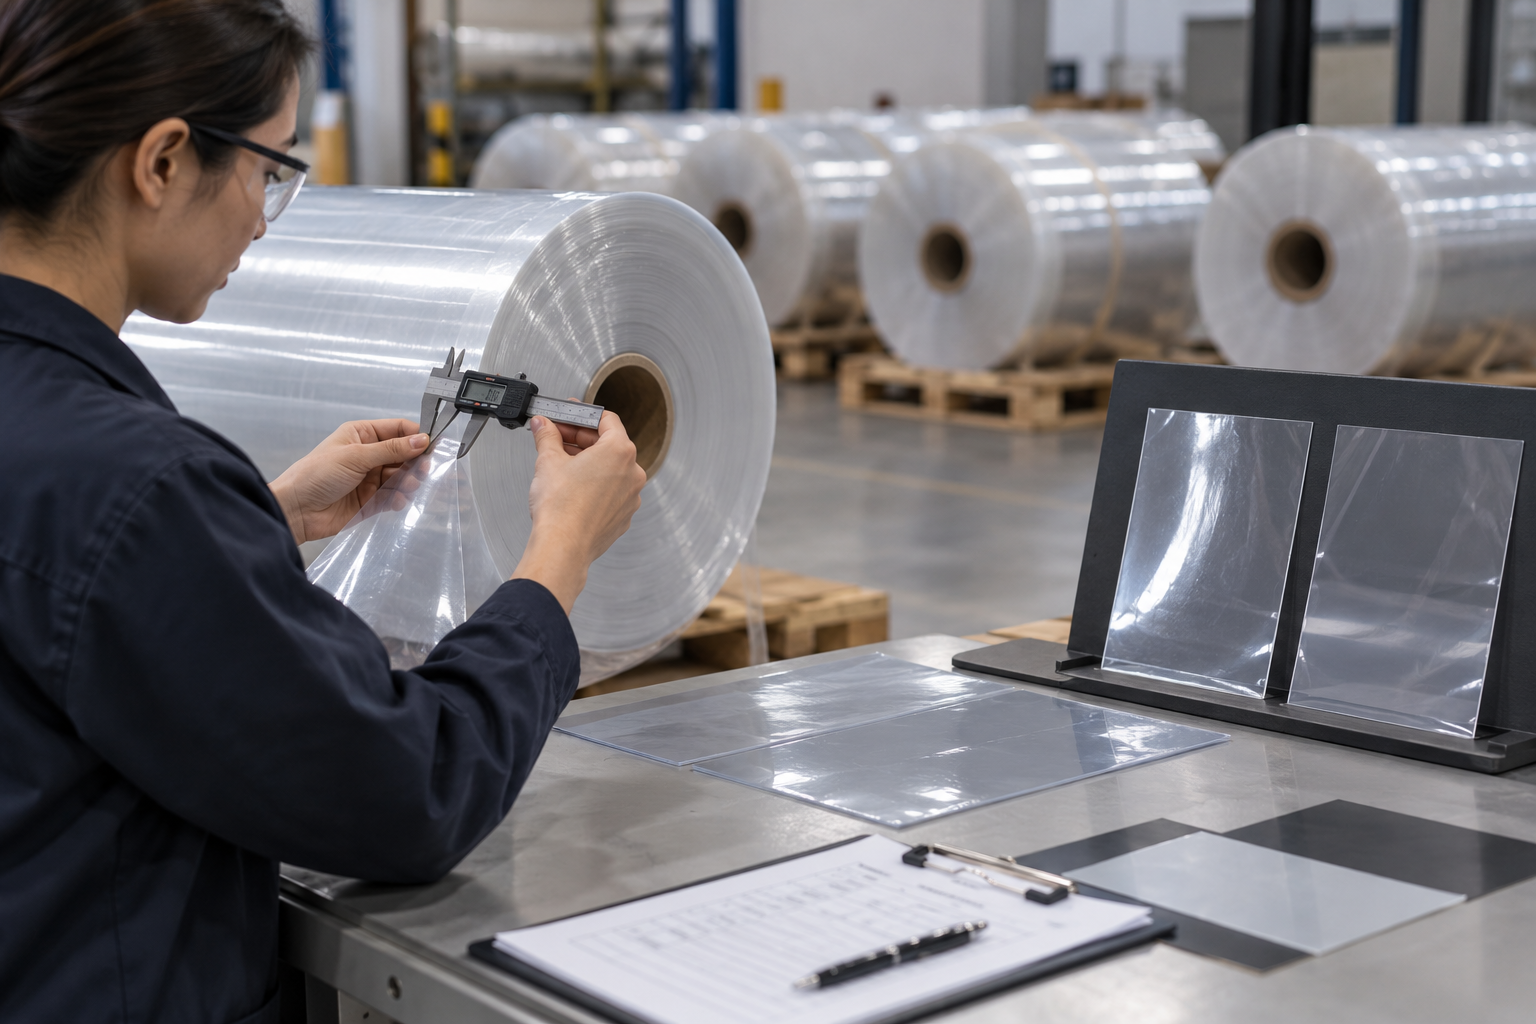
Thickness, width, core dimensions and roll geometry directly affect machine fit and material distribution. Measure them using the same agreed method and sampling positions used for the approved baseline. A single thickness reading near one edge is weak evidence; it cannot show the cross-web or within-roll variation that may affect heating and forming.
Confirm:
- thickness at the defined positions and frequency;
- usable web width;
- core dimensions and core condition;
- roll diameter or other agreed roll-size limits;
- winding direction, if the two surfaces have different functions; and
- telescoping, loose winding, crushed edges or other roll-shape problems.
DESU offers PET and R-PET sheet options in widths from 250 to 1,400 mm and, depending on the selected product, thicknesses beginning at 0.18 mm. Availability should be confirmed for the selected structure, gauge, color and roll format. Those supply ranges do not replace the narrower project specification approved for a particular tool and machine.
Width deserves more attention than it sometimes receives. Excess width can create tracking or trimming problems, while insufficient usable width can compromise clamping or cavity layout. A lower roll price per kilogram does not compensate for higher trim waste or unstable feeding.
Inspect the surfaces and edges under consistent conditions
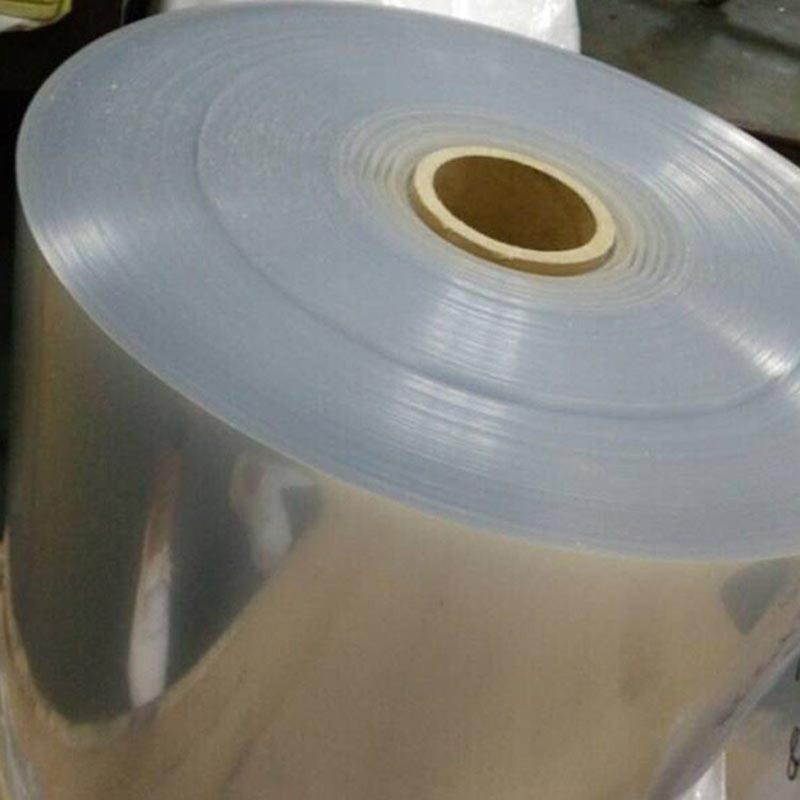
Place the received material beside the approved reference under controlled lighting. Look for differences in color, clarity and general surface condition as well as visible contamination, gels, black specks, scratches, dents, creases and edge damage. Record where an issue appears and how often it occurs instead of describing the whole roll as merely “good” or “bad.”
RPET appearance must be judged against an agreed RPET baseline, not an undefined expectation that every recycled-content sheet will look identical to virgin PET. Recycled content, sheet construction and process control can influence appearance and forming behavior. The commercial requirement therefore needs measurable or reference-based acceptance criteria.
If the project relies on a particular surface treatment or downstream operation, verify that the delivered surface designation matches the order. DESU provides PET/R-PET options such as silicone-oil-coated or embedded anti-block sheet, while corona-treated PET/R-PET is offered for printing applications. The relevant surface should be identified before forming, printing, bonding or sealing trials; visual similarity does not prove downstream compatibility.
Check packaging and handling condition
Packaging damage is not automatically a material defect, but it can expose the roll to contamination, moisture or physical damage. Inspect the outer protection, end guards, pallet or support arrangement and any signs of impact or water exposure. Note the condition before moving the roll so responsibility and subsequent handling are clear.
Allow the material to reach appropriate production-room conditions before drawing conclusions from a cold or recently transported roll. Keep the storage and conditioning approach consistent with the approved baseline. If a problem is suspected, change one factor at a time; simultaneous changes to sheet, heater settings, mold conditions and handling destroy the evidence needed to isolate the cause.
| Check area | What to compare | Why it affects the decision |
|---|---|---|
| Identity | Lot, roll number, material, structure and order reference | Prevents mixed or untraceable material from entering production |
| Dimensions | Thickness profile, width, core and roll size | Confirms machine fit and supports stable material distribution |
| Appearance | Color, clarity, gels, specks and scratches | Protects the approved visual standard for the formed package |
| Roll condition | Winding, edges, telescoping and physical damage | Reduces feeding, handling and trim risks |
| Surface requirement | Correct side and agreed treatment | Supports printing, bonding, separation or other downstream work |
| Packaging condition | Protection, contamination and transport damage | Identifies handling risks before the roll is released |
| Trial behavior | Heating, forming, trimming and output observations | Confirms that incoming conformity translates into usable production |
Keep a Retained Baseline That Production Can Actually Use
A certificate or delivery document can support identification, but neither is a substitute for a retained baseline. The strongest repeat-order reference combines the written specification with a clearly identified sample and production observations from the approved material.
Keep enough information to answer four questions:
1. What material and roll was approved?
2. How was it measured or inspected?
3. Under what relevant machine, mold and handling conditions was it run?
4. What did the formed part and production team observe?
The retained sample should be protected, labeled and linked to its lot and approval date. For appearance-sensitive packaging, a physical limit sample or agreed visual reference is usually more useful than phrases such as “high clarity” or “normal color.” The same principle applies to gels, scratches and other visual features: define what is acceptable rather than relying on memory.
One exceptional sample should not become proof of long-term consistency. In our experience, repeatability across rolls and lots matters more than a single perfect sheet, particularly where shelf presentation or product visibility is central. If the first order was approved from only a small sample, the next sensible step is to strengthen the baseline with evidence from production-scale material.
Do not approve a substitution by polymer name and nominal thickness alone. Two PET or RPET sheets with matching labels can behave differently because their construction, formulation, surface and roll consistency are not identical. We would retain observations from heating, web tracking, forming, cooling, release and trimming, together with representative formed parts.
The baseline should also state the application requirement that drove approval. For example, a produce tray project may need an agreed balance between recycled content, product visibility and forming stability. Without that context, a later team may reject a usable lot for a harmless visual difference—or accept a visually similar lot that creates line instability.
Connect Production Feedback to Each Incoming Lot
Incoming measurements can release a roll for a controlled trial, but they cannot fully reproduce thermoforming. The decisive evidence is whether the material produces acceptable parts under production-like conditions without unacceptable instability, scrap or downtime.
Select a clearly identified roll from the received lot and run it using the approved setup as the starting point. Avoid immediately tuning the machine until the new sheet appears to work. If several settings are changed before the first comparison, the team loses the ability to distinguish material variation from process adjustment.
Record observations that affect usable output:
- web feeding, tracking and roll handling;
- heating response and any unusual adjustment required;
- forming definition and material distribution in critical areas;
- sticking, release or blocking behavior;
- part flatness, stacking or nesting, where relevant;
- trimming quality and trim waste;
- visual condition after forming; and
- stoppages, scrap and operator intervention.
A small temperature adjustment is not automatically proof that the lot is unacceptable. Nor should a roll be accepted merely because acceptable parts were eventually produced. The meaningful comparison is how far the process moved from the approved window and whether the resulting output, stability and quality remain commercially acceptable.
This is where price-only comparisons fail. A lower PET sheet roll price per kilogram can be offset by extra setup time, unstable forming, higher trim loss or reduced usable output. We recommend comparing the repeat order on total production performance, not quotation price in isolation.
When a problem appears, identify the affected roll and preserve evidence before changing multiple variables. Compare another roll from the same lot if appropriate, then a retained or known-good roll under equivalent conditions. This disciplined sequence helps separate a sheet issue from the machine, mold, storage or handling conditions.
Production feedback must return to purchasing and quality in a usable form. “The new roll was difficult” is too vague. “Roll 12 required a materially different heating setting and showed repeated thinning at the same corner under the approved setup” gives the supplier and internal team something they can investigate.
Decision Guidance: Release, Hold or Escalate
The release decision should combine incoming conformity with controlled production evidence.
Release the lot when identity is complete, agreed incoming checks meet the approved criteria and the production confirmation remains within the accepted operating and part-quality baseline.
Hold specific rolls or lots when traceability is incomplete, dimensions or appearance fall outside agreed limits, packaging damage may have affected the material, or production behavior differs without a clear cause.
Escalate for joint technical review when incoming results look acceptable but production behavior has shifted. Share roll identity, measurements, photographs, machine observations and representative parts. That evidence is more useful than a general complaint and reduces the risk of changing the wrong variable.
The most reliable repeat-order control is simple: connect every roll to a defined lot, compare it with the same approved criteria, and preserve the link between incoming inspection and line performance. RPET should not be accepted by material name alone, and it should not be rejected merely because it is RPET. Judge the delivered sheet against the documented requirements of the actual package and process.
FAQ About RPET Sheet Repeat Orders
Is a supplier certificate enough to release a repeat RPET order?
No. A certificate can support lot identity and reported conformity, but release should also include the agreed incoming measurements, visual and roll-condition checks, and production confirmation where forming behavior is critical. The evidence must remain linked to the delivered lot and rolls.
How many rolls should be checked from an RPET shipment?
Use the sampling plan agreed for the project and apply it separately to each represented lot. The number should reflect shipment size, characteristic risk, prior consistency and the consequence of failure. If no sampling plan exists, define one with the supplier before treating a few convenient measurements as representative of the shipment.
Should a repeat order use exactly the same thermoforming settings as the approved lot?
Use the approved settings as the comparison starting point. Minor adjustment may be normal, but record any change and evaluate whether the operating window, output and formed-part quality remain acceptable. Do not change several settings before observing how the new lot behaves against the baseline.
What should be sent to the supplier when a repeat roll forms differently?
Send the purchase order reference, lot and roll identity, relevant incoming measurements, photographs, storage and conditioning details, machine and mold information, starting settings, adjustments made, defect location and representative formed parts. Keep the affected roll isolated so the observations can be investigated against a known sample.
Discuss an RPET Repeat-Order Baseline With DESU
For a meaningful material review, provide DESU with the approved sheet structure, recycled-content target, thickness and width, roll requirements, package geometry, thermoforming equipment, critical appearance limits and observations from the previous production run. This gives both sides a practical basis for confirming the repeat-order specification and planning any required production-like trial.
Related Articles
- BRIEF VIDEO TO TAKE A LOOK OF OUR PET SHEET FACTORY AND THERMOFORMING PET PRODUCTION LINE WORKSHOP(8yLd7a8aIxo)
- Congratulations Our PP / PET Sheet Sample Past Customer’s Blister/Thermoforming Performance Test(Gn1TT9w7CA8)
- Check The transparent ratio of our GAG PET Sheet product(AhEuh9hu6uA)
- PET Food Grade Blister Sheet Production Line
CONTACT PET-SHEET.COM
Our professional sales staff and technicians will determine the final characteristics of the product and material solution for the customer specific application and will provide the customer with a quote and a detailed time schedule, Please fill the form to contact our professional sales team.- Main Category
- APET Sheet Roll
- ESD Antistatic PET Sheet Roll
- GAG Sheet Roll
- PETG Sheet Roll
- RPET Sheet Roll
- Thermoforming PET Sheet Roll
- Latest Products